Description
ISOARC 307 stainless steel
Characteristics
This electrode is specially formulated to weld at low amperage to ensure minimum distortion. The ISOARC 307 has good ignition and re-ignition properties, good slag removal and minimal loss through spatter. The high recovery rate of 180% ensures fast deposition with a minimum dilution of the base metal.
Applications
ISOARC 307 is used on crossing and points, gears, hot dies, rolls, valves, shafts, gear-teeth, machine parts and heavily loaded welds. Because of its high heat resistant properties, it is ideal as a buffer layer prior to hot working hard-facing applications.
Procedures
Keep the arc short to medium. DO not weave more than three times the diameter of the electrode. Pre-heat up to 250 degrees on steels with poor weldability. Pre-heating is not required for other steels. Always use dry electrodes.
Redrying
Should electrodes become moist re-dry at 350° C for 1 hour
| Classifications | |
|---|---|
| AWS | E307-16 |
| PRODUCT | ISOARC 307 |
| Mechanical Properties | |
| TENSILE | >750-830 N/mm² |
| YIELD | > 480 N/mm² |
| ELONGATION | > 35% |
| Chemical Analysis | |
|---|---|
| Carbon | 0.10 |
| Manganese | 5.00 |
| Phosphorous | max 0.04 |
| Silicone | 1.00 |
| Sulphur | max 0.03 |
| Chromium | 20.0 |
| Molybdenum | 1.0 |
| Nickel | 9.00 |
| Diameter | Length | Current | Pack Mass | Item No |
|---|---|---|---|---|
| 2.5 | 350mm | 90 – 100A | 5kg | EL16625 |
| 3.2 | 350mm | 120 – 180A | 5kg | EL16632 |
| 4.0 | 350mm | 170 – 220A | 5kg | EL16640 |
| 5.0 | 350mm | 190 – 270A | 5kg | EL16640 |
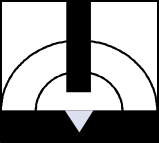
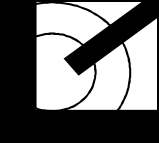
Welding Positions